Yarn Tension Knit Defects: A 300D Tote That Came Back at 0.8%, and the cN Band That Fixed It
Why did a stable 300D rPET tote programme suddenly return 0.8% faults at the inline check? The cause was not the yarn, the needle or the file: it was yarn tension drifting from 14 cN to 31 cN across one cone change, which is outside the 8 to 25 cN working band and above the 1.5 cN tolerance the bed will hold without marking the fabric. This article walks through that run, names the six defects tension produces and the signature of each, then gives the corrective order and the figures a buyer should write into the tech pack.
The Run That Came Back at 0.8%: What the Fabric Showed
A 300D rPET tote at E12 running steadily at 0.2% faults rose to 0.8% within a single shift, and every one of the faults sat in the same place — a horizontal band roughly 60 mm tall, repeating every 340 mm down the body.
The period is the diagnostic clue. A repeating band at a fixed interval points at something cyclical in the feeding system rather than at a random event, and 340 mm on this body corresponds to one full cone traverse. The yarn lot had not changed, the programme revision had not changed and the needle bed had been set up that morning, so the shortlist was tension, humidity and take-down. A handheld tension meter read 14 cN at the start of the run and 31 cN at the point the fault appeared.
Nothing about that run was exotic. Tension drift of this kind happens when a cone is changed and the new package unwinds differently, when a ceramic guide wears, or when the storage feeder is set for a different count. What made it expensive was that the fault was found at the inline check rather than at the bed, so several hundred pieces had already been knitted before anyone measured anything. The fix took under an hour; the rework took two days.
Reading Tension in Centinewtons: The 8 to 25 cN Band
Working yarn tension on a bag-gauge flat knitting bed sits between 8 and 25 cN for a 300D body, and the bed will hold plus or minus 1.5 cN around a set point without marking the fabric — above roughly 25 cN the loops are pulled tight and the surface reads as a barre, and below 8 cN the loops form loose and drop.
Centinewtons are the right unit because the forces involved are small and the tolerance is smaller. A 300D rPET filament yarn has a tenacity around 3.5 to 4.5 cN per dtex, which puts its breaking load far above anything a knitting bed applies; 300 denier is about 333 dtex, so the yarn breaks somewhere near 1,150 to 1,500 cN. Working tension should therefore sit below about 10% of breaking load, and the practical band of 8 to 25 cN is comfortably inside that. The failure mode is never the yarn snapping from tension alone; it is the loop being formed at the wrong size.
Gauge moves the band. A coarse body at E7 in 600D runs at the top of the range, near 22 to 25 cN, because a heavier yarn needs more pull to form a clean loop. A fine body at E14 in 150D runs near the bottom, around 8 to 12 cN, because the same pull on a finer yarn over-forms the loop and can cut it on the needle hook. Setting one band for the whole programme and never revisiting it is the most common source of the drift described above.
- Working band, E12 in 300D
- 14 to 20 cN, set point 16 cN
- Working band, E7 in 600D
- 22 to 25 cN
- Working band, E14 in 150D
- 8 to 12 cN
- Tolerance around set point
- plus or minus 1.5 cN before the fabric marks
- Breaking load, 300D rPET
- roughly 1,150 to 1,500 cN at 3.5 to 4.5 cN per dtex
- Working tension ceiling
- below about 10% of breaking load
Where Tension Is Set: Feeder, Storage Feeder and Take-Down
Yarn tension is set in three places, not one: the cone unwinding at the creel, the storage feeder that normalises what the creel delivers, and the take-down that pulls the formed fabric off the bed — and the storage feeder is the one that actually decides whether the cone's behaviour reaches the needle.
The creel is the noisiest part of the system. A cone unwinds with more resistance at the start of a package than at the end, and side-unwinding packages vary as the traverse crosses the package. The storage feeder exists to absorb that variation: it holds a small reserve of yarn on a drum and delivers at a controlled rate, so what reaches the needle is decoupled from what the cone is doing. Where a storage feeder is set for the wrong count, or its drum is glazed, the decoupling fails and the cone's variation arrives at the needle intact. Take-down is the third element. Fabric tension as the piece leaves the bed affects loop formation at the needle, and on a whole-garment body with varying width, take-down has to be programmed to follow the width or the narrow sections will be over-tensioned.
- Creel: cone angle and unwinding resistance vary across a package; check guides are ceramic and unworn.
- Storage feeder: the component that decouples cone behaviour from the needle; set it for the actual count in use.
- Positive feed: delivers a fixed yarn length per course, which holds stitch density more tightly than tension alone.
- Take-down: must follow body width on a shaped piece, or narrow sections knit tighter than wide ones.
- Needle hook and latch condition: adds resistance locally, so a single worn needle produces a vertical fault line.
The Six Defects Tension Produces, and the Signature of Each
Tension problems present as six recognisable defects — dropped stitches, barre, needle lines, loop burst, skew and GSM drift — and each has a distinct geometry that identifies it faster than any instrument, because the shape of the fault tells you which element of the feeding system failed.
| Defect | Geometry on the fabric | Tension cause | First correction to try |
|---|---|---|---|
| Dropped stitch | A vertical ladder of unclosed loops | Tension too low at the moment of loop formation, below 8 cN | Raise set point by 3 cN and re-check loop closure |
| Barre | Horizontal band repeating at a fixed interval | Cyclical variation of more than 1.5 cN around the set point | Check the storage feeder and the cone traverse |
| Needle line | A single vertical line of tight or loose loops | Local resistance at one needle, often a worn hook or latch | Replace the needle, then re-measure at that position |
| Loop burst | Small hole with broken filaments around it | Tension above 25 cN on a fine yarn, cutting on the hook | Lower set point, confirm the count matches the setting |
| Skew or bow | Courses running off square across the width | Uneven take-down across a shaped body | Re-programme take-down to follow the body width |
| GSM drift | Finished weight outside plus or minus 2% | Stitch density changing with tension over a long run | Log tension every 2 hours and correlate against GSM |
The geometry matters because it directs the correction to the right element. A vertical fault is a single-needle problem and is fixed at the needle. A horizontal repeating fault is a feeding-system problem and is fixed at the feeder or the cone. A fault that appears across the whole width equally is a set-point problem, not a component problem, and moving individual components will waste the shift without changing the fabric.
Environment: 65% RH, 22 to 25 °C, and Wax at 3%
Tension cannot be held without environment control: a knitting room held at 22 to 25 °C and 65% relative humidity, plus or minus 5%, plus wax pick-up near 3% by mass, is the precondition for any tension setting being repeatable from one shift to the next.
Humidity changes yarn friction, and friction at the guide is read by the yarn as tension. Below about 55% RH a polyester filament builds static and drags; above about 75% RH a hygroscopic fibre such as nylon or a cotton blend swells and drags differently again. Wax is the counterweight. Applied at roughly 3% by mass during cone winding it stabilises the coefficient of friction across the whole package, which is why the yarn-preparation station exists at all rather than cones going straight to the creel. Temperature matters less than humidity but is worth holding, because a cold room changes the behaviour of the lubricant on the needle bed.
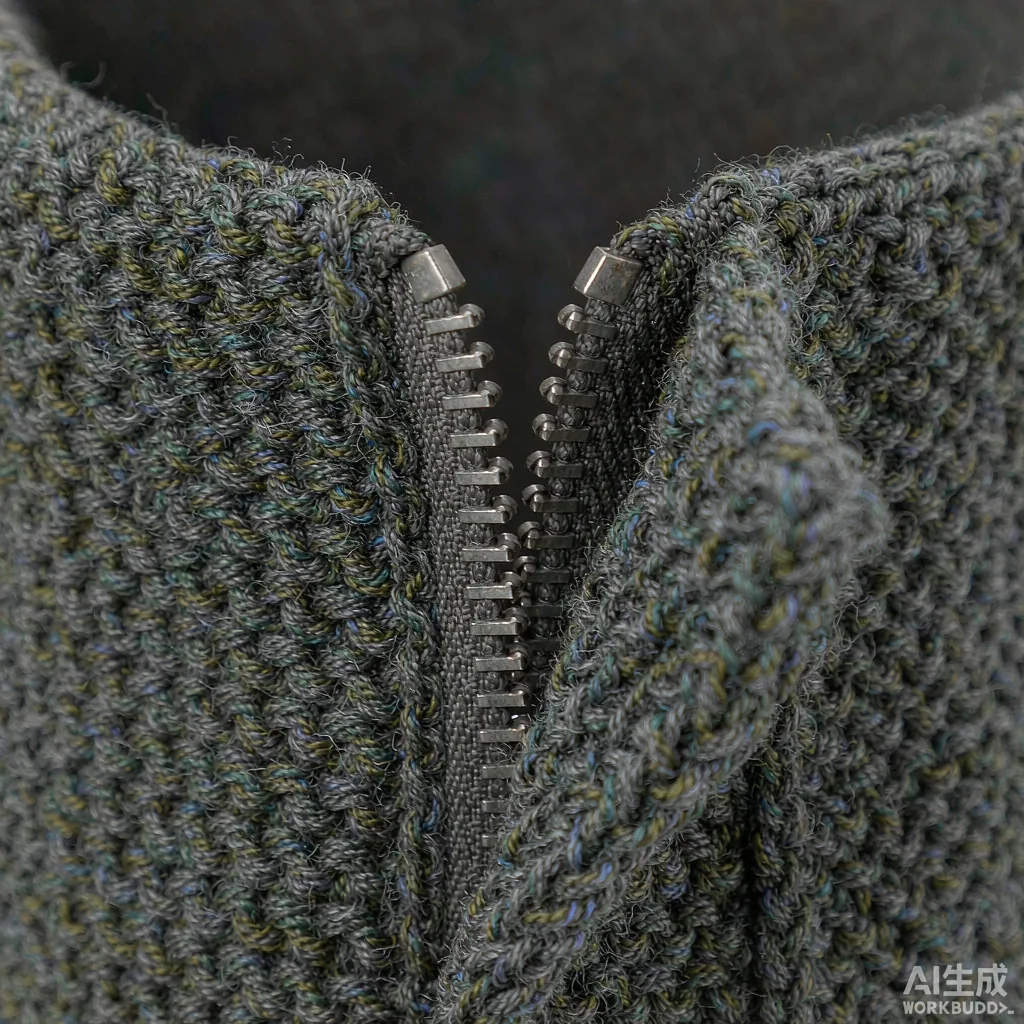
Measuring Tension: Instrument, Frequency and Record
Tension is measured with a handheld electronic tension meter read at eight positions across the bed every two working hours, and the reading is logged against the piece count — because a single reading tells you nothing, while a logged series tells you which element drifted and when.
Eight positions is the practical minimum on a bag-width bed: two near each selvedge, two at the quarter points and two at the centre. Reading only at the centre misses the most common failure, which is a positional gradient caused by one worn guide on one feeder. Two-hour intervals catch drift before it becomes a fault, given that a bed running a 9-minute cycle produces roughly 13 pieces in that window. The record should carry the piece count, the position, the reading and the set point at that moment, so a fault found at the inline check can be traced back to the exact run segment that produced it.
Tension record: what to log
- Set point in cN for the gauge and count in use, restated at every cone change
- Reading at eight positions across the bed, every two working hours
- Piece count at the time of reading, so a fault can be traced to a run segment
- Room temperature and relative humidity logged on the same sheet
- Cone lot reference, because a lot change is the most common cause of a step in the series
- Action taken, so a correction that worked is not re-derived from scratch next time
Corrective Sequence: What to Change, and in What Order
When tension drift is confirmed, change one thing at a time in a fixed order — cone and guides first, then storage feeder, then set point, then take-down, then needles — because changing two elements together destroys the diagnostic and the run has to be repeated to find out which one mattered.
The order follows the cost of the change rather than its likelihood. Cone and guides are free and take minutes, so they go first. The storage feeder setting is next, and on this programme it was the answer: the feeder had been left set for a 600D run and was delivering 300D with the wrong wrap, which raised tension from 14 cN to 31 cN at the fault point. Set point comes after the feeder, because adjusting the set point to compensate for a wrong feeder setting produces a fabric that measures correctly and behaves badly. Take-down and needles come last, because both require the bed to be stopped.
On the run described at the top, correcting the feeder setting returned tension to 16 cN, and the fault rate fell from 0.8% to 0.2% within 40 pieces. The two days of rework were the cost of finding it late, not the cost of fixing it. This is the entire commercial argument for logging tension on a schedule: the measurement costs almost nothing, and the alternative is discovering the same drift at the inline check several hundred pieces later.
Holding the Fix: Tension Inside the AQL 2.5 Defect Plan
Tension faults are classified by how they affect use rather than by how they look, so a barre that is visible at arm's length is a major defect under an AQL 2.5 plan, while a dropped stitch at the handle root is critical regardless of how few pieces carry it.
That classification is what turns a tension problem into either a re-knit or a rejected shipment. Under an ISO 2859-1 sampling plan at AQL 2.5, the sample size and the accept and reject numbers are fixed by the lot size; what is not fixed is the defect classification, and it should be agreed in writing before production rather than argued at the carton. A programme that logs tension every two hours and correlates it against GSM can also demonstrate that a fault was confined to a known run segment, which is often the difference between re-inspecting one segment and re-inspecting the whole lot.
What a Buyer Should Write Into the Tech Pack
The three figures worth specifying are the working tension band in cN, the tolerance around the set point, and the measurement frequency and position count — because a tech pack that states gauge, count and GSM but not tension leaves the variable that caused the fault unmanaged.
A workable clause names the band for the gauge and count in use, states the tolerance as plus or minus 1.5 cN, requires a reading at eight positions every two working hours, and requires the log to be produced if a defect is found. It should also name the environmental band of 22 to 25 °C and 65% relative humidity, plus or minus 5%, and the wax pick-up near 3%, since without those the tension figure is not repeatable between shifts. Alongside it, the pack should carry GSM at plus or minus 2% and the dimensional tolerance of plus or minus 3 mm on a 380 mm body, both measured after heat setting under the conditions described in steam boarding and heat setting. MOQ is 100 pcs per style or colourway, sampling runs to 7 working days, bulk to 30 days, and FOB Xiamen is the standard term.
Get a tension spec written into your tech pack
Send the gauge, the yarn count and the target GSM. Our knit team will return a working tension band in cN, a measurement schedule and a defect classification, quoted against MOQ 100 pcs per style, 7 working days of sampling and 30 days of bulk production. Start on the contact page.
Frequently Asked Questions
What yarn tension should a knitted bag run at?
Between 8 and 25 cN depending on gauge and count. A 300D body at E12 runs at 14 to 20 cN with a set point near 16; 600D at E7 runs at 22 to 25 cN; 150D at E14 runs at 8 to 12 cN. The bed holds plus or minus 1.5 cN around the set point before the fabric starts to mark.
What unit is yarn tension measured in?
Centinewtons, written cN. The forces at a knitting feeder are small and the tolerance is smaller, so newtons are too coarse to be useful. A handheld electronic tension meter reads directly in cN and is the standard instrument for setting and checking a bed.
How does tension cause a dropped stitch?
When tension falls below about 8 cN the loop is not pulled closed on the needle hook, so the old loop slips off before the new one is formed and a vertical ladder appears. Raising the set point by 3 cN and re-checking loop closure is the first correction, before any component is changed.
What is barre and what causes it?
Barre is a horizontal band of visibly different loop density repeating at a fixed interval down the fabric. It is caused by cyclical tension variation of more than 1.5 cN, most often from a storage feeder set for the wrong yarn count or from a cone traverse. It is a feeding-system fault, not a yarn fault.
How is a needle line different from barre?
A needle line is a single vertical line of tight or loose loops caused by local resistance at one needle, usually a worn hook or latch. Barre is horizontal and cyclical. The geometry directs the correction: vertical means replace the needle, horizontal repeating means check the feeder and the cone.
Why does humidity affect yarn tension?
Humidity changes yarn friction, and friction at a guide is read by the yarn as tension. Below about 55% relative humidity a polyester filament builds static and drags; above about 75% a hygroscopic fibre swells and drags differently. Holding 65%, plus or minus 5%, is what makes a setting repeatable.
How often should tension be measured during a run?
Every two working hours, at eight positions across the bed, logged against the piece count. A bed on a 9-minute cycle produces about 13 pieces in that window, so drift is caught before it becomes a fault. Two positions near each selvedge, two at each quarter point and two at the centre.
What is a storage feeder and why does it matter?
A storage feeder holds a small reserve of yarn on a drum and delivers at a controlled rate, decoupling what the cone is doing from what the needle receives. A cone unwinds differently at the start of a package than at the end; without the feeder that variation reaches the loop intact and shows as barre.
What order should corrections be made in?
Cone and guides first, then storage feeder, then set point, then take-down, then needles. The order follows the cost and speed of each change. Adjusting the set point to compensate for a wrong feeder setting produces fabric that measures correctly and behaves badly, so feeder comes before set point.
Can tension problems be found before production starts?
Partly. A first-piece check that records tension at eight positions alongside GSM and dimensions will catch a feeder set for the wrong count before the run begins. What it cannot catch is drift within a run, which is why the two-hourly log exists as a separate control.
How are tension faults classified under AQL 2.5?
By effect on use, not by appearance. A barre visible at arm's length is a major defect under the ISO 2859-1 sampling plan; a dropped stitch at the handle root is critical regardless of how few pieces carry it. Agree the classification in writing before production rather than at the carton.
Does tension affect finished GSM?
Yes. Tension governs stitch density, and stitch density governs weight. A long run with slowly rising tension will drift outside the plus or minus 2% GSM tolerance even though every individual piece looked acceptable. Logging tension and correlating it against GSM is the only way to see it coming.
What wax level is used on knitting yarn?
About 3% by mass, applied during cone winding at the yarn-preparation station. Wax stabilises the coefficient of friction across the package, which is what makes a tension setting hold from the outside of a cone to the inside. Below that the yarn scuffs at the feeder; above that it deposits on the needles.
Is a higher tension always stronger fabric?
No. Above roughly 25 cN the loops are pulled tight, the surface reads as barre, and on a fine yarn the loop can be cut on the needle hook, producing filament breakage and holes. Strength comes from the yarn and the stitch structure, not from how hard the loop was pulled.
What should the tech pack say about tension?
Name the working band in cN for the gauge and count in use, state the tolerance as plus or minus 1.5 cN, require a reading at eight positions every two working hours, and require the log if a defect is found. Add the environmental band and the GSM tolerance so the setting is repeatable between shifts.
What happened to the 0.8% fault rate in the example run?
It fell to 0.2% within 40 pieces once the storage feeder was reset for 300D and tension returned to 16 cN. The fix took under an hour. The expensive part was finding it at the inline check rather than at the bed, which is the argument for scheduled logging.
People Also Ask
What is yarn tension in knitting?
The pulling force applied to the yarn between the package and the needle, measured in centinewtons. It governs loop size, and loop size governs stitch density, GSM and the surface appearance of the finished fabric.
Why is my knitted fabric streaky?
Streaks repeating at a fixed interval are barre, caused by cyclical tension variation above 1.5 cN. The usual source is a storage feeder set for the wrong yarn count, so check the feeder before changing the yarn.
Can tension damage the yarn?
Rarely by breaking it, since a 300D rPET yarn breaks near 1,150 to 1,500 cN while the bed works at 8 to 25 cN. Damage appears instead as over-formed loops, cut filaments at the needle hook and a tight, barre-marked surface.
How do you measure knitting yarn tension?
With a handheld electronic tension meter read at eight positions across the bed every two working hours, logged against the piece count. The logged series, not a single reading, is what identifies which element of the feeding system drifted.
Does recycled yarn behave differently on the bed?
A well-specified recycled polyester runs at the same band as a virgin one, but lot-to-lot variation is wider, so the cone lot reference belongs on the tension log. A step change in the readings after a lot change is normal and should be re-set, not ignored.
Sources and further reading
Every figure on this page is either our own programme data or attributed below. Open the originals before you write them into a specification.
- ISO 2859-1:2026 — Sampling procedures for inspection by attributes, Part 1: AQL-indexed sampling schemesISO Defines the sample size and accept or reject thresholds used to classify the tension faults described here.
- ISO 12947-2:2016 — Textiles, determination of abrasion resistance by the Martindale methodISO Referenced because tension-driven stitch density changes shift the abrasion result on the finished body.
- AATCC — American Association of Textile Chemists and ColoristsAATCC Source of the dimensional change and colour fastness methods used alongside the GSM tolerance quoted here.
- Recycled Claim Standard and Global Recycled StandardTextile Exchange Chain-of-custody standard behind the recycled-content documentation tied to the cone lot on the tension log.
- OEKO-TEX STANDARD 100OEKO-TEX Finished-textile testing for harmful substances, requested alongside REACH and Prop 65 on knit bag programmes.
Why the Least Expensive Control Is the One Nobody Buys
A tension meter, a log sheet and a two-hourly reading cost almost nothing against the price of a re-knit. The run described at the top of this article produced a fault that took under an hour to fix and two days to rework, and the entire difference was the point in the process at which somebody measured. Every tension defect in the table above is straightforward to prevent and expensive to find late.
For the variables tension feeds into downstream, see tolerance control on a seamless bag body. For the yarn counts and fibre choices that set the working band, see knit bag materials and yarns.